


OSENC supplies custom titanium nitride coated neodymium magnets engineered as finished magnetic components, not simply gold-colored parts. Our current TiN project framework uses low-temperature PVD, with DC/RF magnetron sputtering and Ti/TiN architectures preferred when the application needs a hard, thin functional surface while controlling magnetic and dimensional risk.
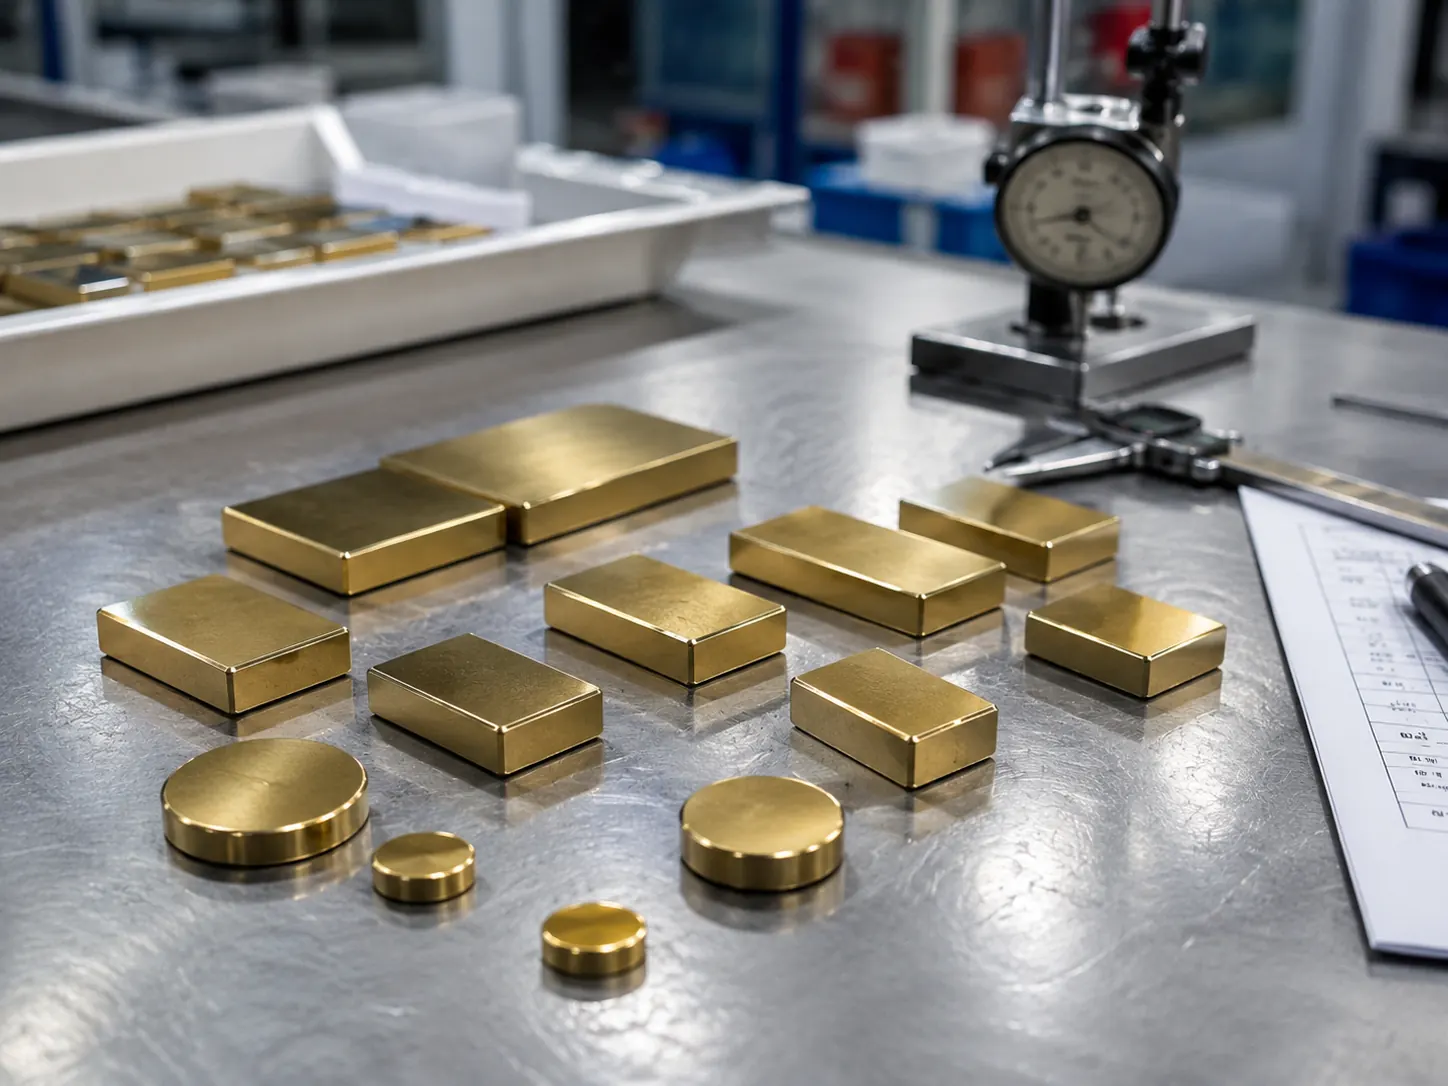
TiN is a thin PVD ceramic coating used when surface wear, tight dimensional build, or another controlled surface function justifies more process control than a conventional magnet coating. For OSENC projects, the coating and NdFeB core are specified as one finished part: grade, geometry, magnetization, TiN stack, coating thickness, final dimensions, temperature exposure and inspection method must agree before production.
TiN is not automatically the best coating for every magnet. Nickel remains a practical industrial default, epoxy is useful where a polymer barrier is preferred, and Parylene can be valuable for thin conformal coverage. OSENC uses TiN when the application gives a clear engineering reason to use it.
| Parameter | Current Project Framework | Buying Boundary |
|---|---|---|
| TiN process | Low-temperature PVD; DC/RF magnetron sputtering preferred. Cathodic Arc PVD can be evaluated. | Cathodic arc and other higher-energy routes require substrate-temperature and magnetic-loss validation. |
| Coating architecture | NdFeB → Ti adhesion layer → TiN; Ti/TiN multilayer preferred for higher corrosion-control requirements. | Ni-based barrier + Ti/TiN is a development option, not a default stack; adhesion and corrosion must be re-qualified. |
| TiN thickness | 1–5 μm design capability; 2–4 μm typical; 3 μm nominal starting point. | Thickness is locked only after wear, fit, geometry and process review. |
| Thickness control | ±0.5 μm or ±15% can be used as a drawing target. | Qualification target Not a universal default tolerance for every geometry. |
| NdFeB grades | N35–N52 standard range; M/H/SH/UH/EH/AH temperature series available by project. N55/N55M by drawing review. | Final grade depends on operating point, geometry, temperature and coating sequence. |
| Finished tolerance | ±0.05 mm standard; ±0.02 mm precision target. | Tighter micro-part tolerances require dimensional-chain and inspection review; do not assume one tolerance applies to every feature. |
| Shapes | Disc, block, ring, arc, sphere, trapezoid, countersunk, stepped, slotted and custom geometry. | Deep holes, recesses, masks and shadowed areas require separate PVD coverage review. |
| Magnetization | Axial and diametrical are common; block-axis, angle and multipole patterns can be customized. | True radial rings and special pole patterns require grade, geometry and tooling feasibility review. |

Published NdFeB research supports RF magnetron sputtering and Ti/TiN multilayers as technically credible routes for TiN protection. A 2014 study deposited Ti/TiN multilayers directly on sintered NdFeB by radio-frequency magnetron sputtering and reported improved corrosion behavior versus bare NdFeB. A 2021 NdFeB study also showed that substrate temperature materially changes both corrosion protection and magnetic loss, which is why the deposition route cannot be separated from the magnetic specification.
The Ti interlayer provides a controlled transition between reactive NdFeB and the hard TiN surface. For demanding corrosion projects, a Ti/TiN multilayer can be evaluated instead of treating TiN as a single decorative film.
Published PVD TiN studies on different substrates commonly use micrometre-scale films, while a 2023 neodymium-magnet wear study used a 5 μm TiN film. OSENC therefore starts thickness selection from the actual wear, fit and coverage requirement rather than assuming “thicker is better.”
When TiN build affects a bore, slot, air gap or mating interface, nominal thickness alone is incomplete. The drawing should identify measurement locations and the accepted min/average/max or tolerance rule.
Sliding, repeated insertion, fixture contact and handling can justify a hard surface system when coating damage is a real failure mode.
TiN is useful to evaluate where small coating build, repeatable fit and a controlled magnetic gap matter at the same time.
Rotors, couplings, compact actuators and precision mechanisms can benefit when final coated dimensions are more important than a generic plating specification.
TiN-coated NdFeB has published use in vacuum-oriented magnetic systems, but vacuum suitability must be qualified for the actual pressure, cleaning, bake-out, particle and outgassing requirements.
TiN may be considered as one element of a medical or dental component design, but TiN alone does not make a magnet medical-grade, implantable, biocompatible or regulation-compliant. Customer-defined biocompatibility, sterilization and regulatory validation remain mandatory.
Disc, block and ring geometries can be manufactured at sub-millimetre scale, but TiN coverage, edge condition and measurement capability must be re-evaluated as feature size decreases.

| Coating | Best Starting Reason | Critical Review Point |
|---|---|---|
| TiN | Hard, thin functional surface for wear-sensitive, precision or specially qualified environments. | PVD thermal history, adhesion, line-of-sight coverage and coated dimensions. |
| Ni-Cu-Ni | General industrial metallic protection and a practical default for many NdFeB designs. | Mechanical damage, edge exposure and the actual corrosion environment. |
| Epoxy | Polymer barrier when moisture protection is the main design requirement. | Abrasion, sharp edges and local damage can compromise the barrier. |
| Parylene | Thin conformal polymer coating for sensitive and dimension-conscious assemblies. | Thickness, adhesion and application-specific environmental validation. |
OSENC does not force TiN when it adds no value. If a simpler coating meets the real wear, corrosion, fit and cost requirement, the simpler route is usually the better procurement decision.

TiN does not increase the intrinsic magnetic strength or temperature rating of the NdFeB core. The finished result still depends on grade, geometry, intrinsic coercivity, working point, air gap, surrounding steel, magnetization and the coating thermal cycle.
OSENC prefers to complete the TiN process before final magnetization where the product route allows it. For projects that require TiN processing on already magnetized parts, a low substrate-temperature route is preferred. Published NdFeB work found that 100°C deposition gave a useful balance of corrosion protection and lower magnetic-property loss compared with much higher substrate temperatures.
| Failure Mode | Why It Matters | Control Direction |
|---|---|---|
| Pinholes / exposed substrate | Local defects can defeat corrosion protection even when most of the surface looks good. | Define critical faces, visual limits and thickness/coverage inspection. |
| Edge defects or chipping | NdFeB is brittle and edges are vulnerable during machining, coating, handling and assembly. | Control chamfer/edge condition, packaging and coated-finish inspection. |
| Poor adhesion / peeling | A hard coating is useless if it separates from the substrate or interlayer. | Use qualified pretreatment and Ti adhesion architecture; add scratch testing when adhesion is critical. |
| Shadowed PVD areas | Deep holes, slots and recesses may not receive the same line-of-sight deposition as open faces. | Review geometry, masking and functional surface requirements before quoting. |
| Dimension interference | Micrometre-scale coating build can still change fit in precision bores, slots or magnetic gaps. | Dimension the finished coated part and identify inspection locations. |
| Thermal magnetic loss | Unsuitable deposition temperature can reduce magnetic performance even when the coating looks acceptable. | Use low-temperature processing and pre/post magnetic verification when required. |
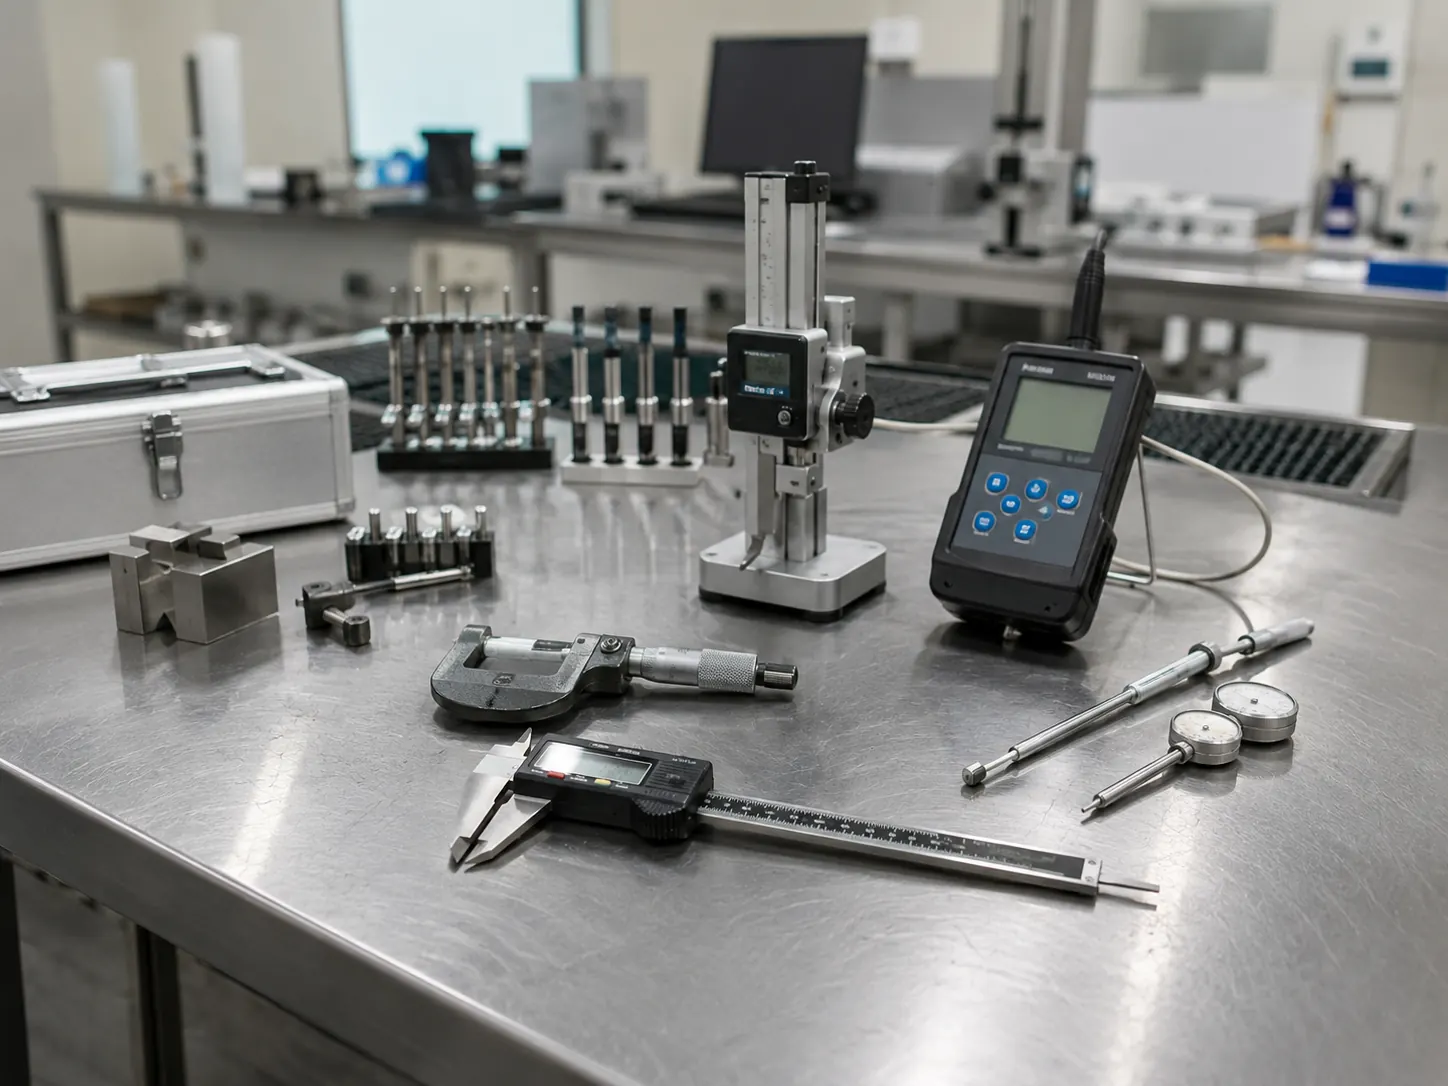
A gold surface is not an inspection result. OSENC builds the quality plan around measurable finished-part requirements and separates routine production checks from development or first-article qualification.
| Item | Recommended Method | Acceptance Rule |
|---|---|---|
| TiN thickness | Production: XRF calibrated to the TiN/substrate system. FAI or validation: cross-section SEM or optical profilometry. | Report measurement locations plus Min / Average / Max against the drawing. |
| Adhesion | Progressive-load scratch test, recording Lc1/Lc2 when adhesion is functionally critical. | Suggested start Lc2 ≥15 N may be proposed for development; final limit requires sample validation. |
| Corrosion | ASTM B117 salt fog when salt-spray performance is relevant. | 24 / 48 / 96 h checkpoints can be defined. No universal salt-spray-hour claim applies without a project requirement. |
| Wear | Project-specific sliding test. One development protocol can use 6 mm Al₂O₃ ball / 5 N / 10,000 cycles / dry room-temperature sliding. | Qualification protocol Record friction, wear track and coating breakthrough; not a default production test. |
| Magnetics | Gaussmeter for flux density; Helmholtz coil for total flux; BH tracer/permeameter for material curve; pull force on a separate force setup. | Method, fixture, gap, orientation and pass/fail limit must be defined. |
| Appearance | Visual inspection under agreed lighting/magnification. | No exposed substrate, peeling, blistering or through-coating scratches on controlled faces. Numerical pinhole, edge-chip or ΔE limits are drawing options, not universal standards. |

Confirm grade, finished dimensions, magnetization, coating faces, masked areas, temperature, assembly fit and the reason TiN is specified.
Confirm PVD route, Ti/TiN structure, target thickness, coverage risks and whether special adhesion, wear or corrosion qualification is needed.
A useful FAI can include Drawing No./Revision, Lot No., five-piece dimensional results, TiN Min/Avg/Max, magnetic result, appearance and PASS/FAIL.
The approved drawing, sample condition, inspection method, lot identification and packaging become the repeat-order reference.
Send the finished-part requirement, not only “NdFeB + TiN.” A complete RFQ lets OSENC review feasibility before the coating, magnetic and dimensional requirements start contradicting one another.

OSENC uses a low-temperature PVD project route, with DC/RF magnetron sputtering preferred and Ti/TiN structures available. The exact process depends on geometry, thermal sensitivity, coating thickness and the required surface function.
OSENC currently uses 1–5 μm as the TiN design window, 2–4 μm as the typical starting range and 3 μm as a practical nominal starting point. The released thickness and tolerance must still be approved for the actual geometry and service condition.
Yes. Even a micrometre-scale film adds coating build. Critical dimensions should therefore be defined and inspected in the finished coated state, especially for bores, slots, precision fits and magnetic gaps.
No. TiN changes surface behavior; it does not increase the intrinsic magnetic properties or automatically raise the operating-temperature capability of the NdFeB grade.
They can be evaluated for vacuum projects, but coating name alone is not a vacuum qualification. The actual pressure, outgassing, cleaning, bake-out, particle and assembly requirements must be reviewed.
They can be evaluated as components in a medical or dental development project, but TiN alone does not make the finished magnet medical-grade, implantable, biocompatible or compliant. Regulatory, sterilization and biocompatibility requirements must be defined and validated by the customer project.
For production, XRF can be used when calibrated to the actual TiN/substrate system. For first-article or validation work, cross-section SEM or optical profilometry can provide stronger thickness verification. The report should state the measurement points and Min/Avg/Max.
If adhesion is critical, use a defined method such as a progressive-load scratch test and agree the Lc1/Lc2 acceptance before production. A suggested engineering target is not the same as a universal product guarantee.
No. The hard ceramic coating discussed on this page is titanium nitride (TiN). “Titanium nitrate” is commonly a terminology error in magnet coating searches.
Published sources below support general engineering statements about TiN on NdFeB, PVD TiN thickness, temperature effects and Ti/TiN multilayers. They do not replace an OSENC drawing, first-article record, batch inspection report or customer-specific qualification.
Technical review: OSENC Magnet Engineering Team · Updated August 30, 2026.
Send your drawing, finished tolerances, grade or magnetic target, pole direction, TiN thickness requirement, operating temperature, service environment, inspection needs and quantity. OSENC will review the complete magnetic component and return a quotation against a controlled finished-part specification.
Get an Engineering Quotation